Services
From development of the formulation to finished product
Formulation
We at Sparta Pharmaceuticals will assist by turning your product idea into an opportunity with viable product formulation taking into account your budget, target audience and required dosage. Once your active ingredients per dosage have been determined, our factory manager will initiate a trial batch to ensure that the correct weights and active distribution of active raw materials is in line with the required specification. Inactive ingredients are added to create a production ready formulation which allows the product to run efficiently on the production equipment. A master batch manufacturing document is drafted and kept on file. Products are manufactured according to their respective batch manufacturing document and all activities during the manufacturing process are documented to allow traceability throughout the batch.
Concept
Turning your product idea into an opportunity with viable product formulation
Fully Outsourced Model
We specialise in handling your product from order to delivery and everything in-between.
Procurement
Our raw materials are sourced from ISO9001 validated suppliers globally to meet the customer’s as well as our own standards. All suppliers are audited by our Quality Control department annually. Once an order has been received from the client, our internal system will locate stock of raw materials and components within our warehouse and allocate them to the forthcoming batch. Any shortages will be ordered from validated suppliers.
Packaging
Our in house design team can assist with the design of your product or brand. From labels, to shrink sleeve labels, to shrink neck sleeves and final cartons. It can all be done in-house.
Packaging Design – Clients can choose from a wide selection of packaging from our samples available.
Private Label – We offer our clients access to hundreds of validated product formulations owned and developed by us for white label branding.
Packaging Examples


Home
We strive to manufacture complimentary medicines, health products and convenience foods to the highest standard available. Customer satisfaction is paramount for the success of our business and we place high importance on building long lasting relationships with our customers.
We strive for perfection in everything that we do, from the cleaning of our equipment, to the finish on our tablets right to ensuring that the labels are straight on the containers.
Our staff are the engine of our business and without an engine we’d go nowhere. High job satisfaction scores ensure our human capital remains strong and motivated.
50%
GROWTH IS KEY
Sparta Pharmaceutical year on year increase in revenue
"What do you need to start a business? Three simple things: know your product better than anyone, know your customer, and have a burning desire to succeed."
— Dave Thomas, Founder of Wendy’s
At Sparta Pharmaceuticals we provide a unique and complete service whereby we assist you in creating your new product from scratch. From the development of the formulation, to the design of your label, selection of your packaging and right the way to the finished product.
Tablets – With a capacity of 10,200,000 tablets per month across many different shapes and tool sizes on hand.
Tablet Film Coating – With a capacity of 3,500,000 – 25,000,000 per single shift per month (Depending on tablet size and shape).
Gel Manufacturing – We have begun manufacturing hydro-alcoholic based gels according to a base formulation which we have developed which assists active ingredients.
Powder Blending – The production capacity per line will be 5000 – 8000 containers (200g – 6kg) per single shift. Batch sizes are 1000+ units


We cater from small to large batch sizes, from start-up companies through to established businesses.
We operate an open book costing strategy which allows for transparency from raw material procurement, to production and onto finished goods cost. This strategy allows for the full understanding of the cost drivers associated with your product.
"In 2008 I was told that I am mad for starting a business during a recession. Fast forward to 2018 and we are moving to a 3700m2 factory where we will build our dream facility to manufacture larger volumes of products for our clients whom we call family."
- Chris McWilliams, Director
Facility
October 2018 – Addition of a new solid dose packing line for packing tablets and capsules into containers.
November 2018 – Independent procurement department established to handle incoming raw materials and components from over 100 suppliers.
December 2018 – The relocation to our new 3500 m2 factory. 20 Plane road Spartan.
January 2019 – Quality Management System (QMS) to be fully implemented.
February 2019 – Pharmaceutical GMP spec 2.5mm epoxy floor to be completed in the new manufacturing facility.
March 2019 – New powder blending plant and packing line to be installed in the new manufacturing facility.
Machinery
October 2018 – We acquired a new automated solid dose packing line capable of +- 7500 bottles per day (Total capacity 15 000 bottles per day).
December 2018 – We acquired a new Nauta powder mixer capable of batch sizes 500 – 1500 kg with a daily capacity of 3000 – 4500 kg per day.
New ingredients
We have begun product trials utilizing the following patented ingredients:
- Teacrine
- Glycopump
- Amentopump
- Agmapure
- Cocoabuterol
- GBBGO
Contact us for support, quote, or general inquiries.
Our administration office will be happy to contact you about advanced inquiries and to address you to our expert office:
Unit B04 Grader Place, 23 Grader Road
Spartan
Gauteng
Johannesburg
1619
Services
From development of the formulation to finished product
Formulation
We at Sparta Pharmaceuticals will assist by turning your product idea into an opportunity with viable product formulation taking into account your budget, target audience and required dosage. Once your active ingredients per dosage have been determined, our factory manager will initiate a trial batch to ensure that the correct weights and active distribution of active raw materials is in line with the required specification. Inactive ingredients are added to create a production ready formulation which allows the product to run efficiently on the production equipment. A master batch manufacturing document is drafted and kept on file. Products are manufactured according to their respective batch manufacturing document and all activities during the manufacturing process are documented to allow traceability throughout the batch.
Concept
Turning your product idea into an opportunity with viable product formulation
Fully Outsourced Model
We specialise in handling your product from order to delivery and everything in-between.
Procurement
Our raw materials are sourced from ISO9001 validated suppliers globally to meet the customer’s as well as our own standards. All suppliers are audited by our Quality Control department annually. Once an order has been received from the client, our internal system will locate stock of raw materials and components within our warehouse and allocate them to the forthcoming batch. Any shortages will be ordered from validated suppliers.
Packaging
Our in house design team can assist with the design of your product or brand. From labels, to shrink sleeve labels, to shrink neck sleeves and final cartons. It can all be done in-house.
Packaging Design – Clients can choose from a wide selection of packaging from our samples available.
Private Label – We offer our clients access to hundreds of validated product formulations owned and developed by us for white label branding.
Contract Manufacturing
At Sparta Pharmaceuticals we can supply, fill and final pack capsules into bottles
Capsules
Supply, fill and pack capsules into bottles.
We utilise two semi-automatic capsule filling lines with a combined single shift monthly capacity of 5,100,000 capsules per month across size 1, 0 and 00 capsules. All filled capsules are polished as they come off the machine to prevent unwanted powder on the exterior of the capsule which can affect product stability and palatability. In process checks are conducted at regular intervals to ensure that the product meets the correct fill weight, disintegration time as well as the correct capsule length when locked.
Tablets
Compress, polish, coat and pack tablets into bottles.
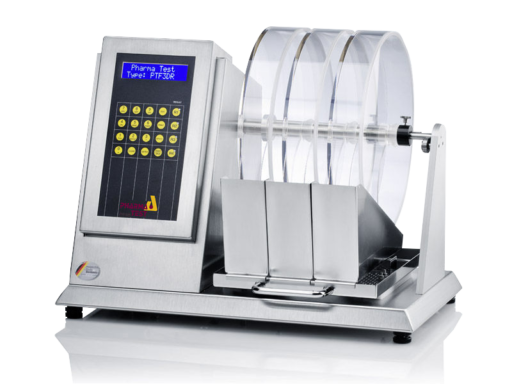
We utilise two automatic compression machines which provide a combined single shift monthly capacity of 10,200,000 tablets per month across many different shapes and size tools on hand. In process checks are conducted at regular intervals to ensure that the product meets the correct weight (to ensure correct amount of raw materials per tablet), disintegration time (time taken to breakdown in the stomach or digestive tract), hardness (prevent breakage) as well as the correct friability (wearability inside the bottle).
Tablet Film Coating
Applying polymer coatings to tablets for the functions of ease-of-swallowing, functional slow release coatings and enteric coating of hygroscopic materials.
Our state of the art 48 inch automatic film coater is capable of coating 120 – 130 kg of tablets every 3-4 hours giving us a capacity of 2 batches per day. This translates into a monthly capacity of approximately 3,500,000 - 25,000,000 per single shift month depending on tablet size and shape.
Ensuring the quality of your Product
Quality assurance and QA regarding procurement and manufacturing.
Conditions and Regulatory
Structural Improvements
Quality Control Systems
Analyze and Evaluate
Staff Training
Upload & Share
Our Process
- Raw materials and components are procured strictly from pre-audited and approved suppliers.
- Once incoming raw materials and components are received they are transferred to Quarantine until such time as they are checked and marked “APPROVED” by Quality Control and moved into the storage area. Raw material Certificates of Analyses is compared with the product sample which is taken and submitted to the retention sample store.
- Raw materials and components are drawn from the stores according to the requirements stated on the batch document.
- Raw materials are dispensed in the dispensary and sealed whilst awaiting QC to double check each dispensed materials weight and whether it is in-line with the batch document requirements.
- Raw materials are transferred to the blending station where they are adequately sieved to ensure the correct particle size and then blended for sufficient time until evenly blended.
- The blended product can now be transferred for encapsulation, tableting or powder filling.
- In-process controls are performed periodically to check whether the product complies to moisture level, tablet weight, tablet thickness, tablet hardness, tablet disintegration, capsule fill weight, capsule length.
- A primary packing line is selected for the packing process.
- QC checks whether the product is being packed into the correct packaging materials.
- Once the product is sealed it is transferred to the secondary packing line for heat induction sealing, labeling/shrink labeling, batch-coding, cartoning and final packing into shippers or palletized.
- Once the batch is quantified and is within an acceptable loss-rate, it is signed off by production and handed over to QC for final acceptability test. QC will draw a retention sample to keep for future reference if there are batch tests required.
- The batch can now move into the finished goods store for dispatch to the client.
98%
Of customers are satisfied with our professional support
100+
White label solution formulations available for your next new product
80%
Quotation approval on submission to clients
Our Team
Informed Creativity
Our management structure with a combined 80 years of industry experience allows us to understand what it takes to bring your product to market at the best possible price, providing a quicker than market average turnaround time whilst maintaining the highest quality assurance levels possible.
Our staff complement of 30 members is growing each quarter and we are fully geared to take your product and business to new heights.
Our Mission
We manufacture for some of South Africa’s most loved brands in the food products, sports nutrition, health products and complimentary medicine sectors.
We strive to continuously improve our policies, procedures and practices.
We will continue to increase our portfolio of services, customers and brands!
Meet the Team
We will continue to increase our portfolio of services, customers and brands!

About Us
Receiving: All received materials and components must be transferred into the quarantine area before they are sampled, quarantined labels to materials or components containers.
Sampling method and procedure for materials: If less than two bags/containers of material received the must be sample individually. If more than two bags/containers received sample every second one. Compare visually the sample material with the retention sample if rejected transfer into the rejected area and stick a rejected label if accepted stick a release label over the quarantine one and transfer the R/Materials into stores.
Sampling method and procedure for components: Open every second box and take a sample of all components received. Compare visually the sample material with the retention sample if rejected transfer into the rejected area and stick a rejected label if accepted stick a release label over the quarantine one and transfer the component into stores.
Dispatch: Upon batch completion, each batch document must be checked and signed off by assistant production manager as well as by Quality Control Manager prior to release. A physical inspection must also be carried out by Quality Control.
Internal in-process checks (IPC): Each manufacturing or packaging document specifies what checks are to be performed by online operator and IPC controller during the manufacturing or packaging of the product. If any of the specified checks are out of the recommended parameters on the document the IPC inspector must stop the (mixing/compression/ encapsulation/coating or packaging of the product and contact the Factory Manager.
Supplier audits: All suppliers need to be audited before approval and authorisation and the name added into the approved supplier list of suppliers to allow procurement to purchase from them in future.
Customer Complaints: If any complaints are received from a customer they must be entered into the complaints book with all the relevant information supplied by the complainer. An investigation must be performed by the Quality Manager and the Factory Manager to establish what is the cause of the problem, and a corrective action report must be complied insuring and preventing the re-occurrence of the same problem in future.
Returns Policy: Should the customers reject any batches for any reason the batch must be returned to Sparta Pharma and stored in the quarantine area where an investigation will performed to establish the reasons the batch is returned. A corrective action must be taken to ensure the issue is corrected and the customer is notified of the outcome.
Key Performance Indicators (KPI’s)
Audited Suppliers: Raw-Materials and Components suppliers may only be added into the approved suppliers list after an audit is performed and approved by the Quality Manager.
Factory Manager
Production Yield: Loss on components and raw materials per batch must not exceed the 5% of the total batch output.
Output: The average output per packaging line must equal or exceed from 3000 – 6000 units per single shift.
Non-conformance: The purpose is to ensure that no unnecessary changes must be made and that all changes are documented on the batch manufacturing or packaging documents. Only the Factory Manager can decide and approved any corrective action.
New product development: The responsibility of the Factory Manager is to assess any new formulations brought by the Chief Executive Officer and decide if a trial batch will be initiated before creating a batch manufacturing and packaging documents.
Planned preventative maintenance: The Factory Managers duty and responsibility to ensure that the maintenance contractor adheres to the preventative maintenance schedule on a monthly basis. In the instance of a breakdown the Factory Manager responsibility is to called out the maintenance contractor to assess the damage and repair.
Stock control: The Factory Manager must ensure that stock count of raw materials and components is performed every quarter by the stores personnel and if any shortfalls must be reported to the Chief Executive officer.
Turn-around Time: Procurement must ensure that all materials and components must be received on a timeous basis as to prevent holding back the production schedule.
On-Time Delivery: Each material and component must be tracked according to purchase order number and supplier and the estimated time of delivery stated by the supplier upon order placement (receiving must not exceed 15 days).
Price Qualification: New quotations must be compared to historical costs as per Pastel Accounting to ensure that the new price falls within 5% of the average historical coat. Should this new price exceed the 5% increase in cost then the procurement personnel must request authorization for the purchase from the Factory Manager or Chief Executive officer.
Chief Executive Officer
Sales: Sales to new and existing customers are facilitated by the CEO.
New business development: The CEO implements all tasks and processes to develop and implement growth opportunities within the company.
New product development: All new product development is steered by the CEO from packaging selection, label artwork, carton artwork, package insert artwork, branding and marketing content. The CEO must sign off on all artwork before manufacturing and packaging commence.
Product Costing: The CEO gathers all material and component quotations via procurement to put together the product costs for potential new or current businesses. These approved finished good costs are given to the administration department to be forwarded to the customer in the form of a sales order.
Quality Manager
Receiving: All raw materials and components received must be allocated to a quarantine area whereby they must undergo sampling by the sampling personnel.
Sampling: The sampling personnel must follow the recommended sampling method as specified on the sampling SOP for raw materials and components by visually compairing the sample taken with the retention sample. If raw material or components rejected transfer them into the rejected area and stick a rejected label and notify the Quality Manager and Factory Manager. If accepted stick a release label over the quarantine one and transfer into the specified stores.
Dispatching: The Quality Manager must conduct a physical inspection of the completed manufacturing and packaging documents and check the IPC checks are compliant with the documents specifications before the product can be released for dispatching to the customer.
Internal process checks: The Quality Manager must ensure that the IPC inspector is performing the in-process checks as specified on the manufacturing and packaging documents.
Supplier audits: Each supplier must be audited annually by the Quality Manager.
Complaints: The Quality Manager responsibility is to manage all product complaints, by retrieving the problematic stock, and investigating the root of the problem and then initiate a non-conformance report and a corrective action change control.
Maintenance
Planned preventative maintenance: All equipment in manufacturing and packaging areas must be checked and evaluated by maintenance personnel a list of preventative maintenance for each machine must be given to the Factory Manager to create a monthly schedule to ensure the preventative maintenance is performed accordingly.
Breakdown maintenance: The Factory Manager must notify the maintenance personnel of a break breakdown immediately and log an appointment to repair the equipment.
Assistant Production Manager
Production yield: Assistant Production Manager must monitor each production department to ensure that the line does not exceed 5% loss during all manufacturing and packaging processes. Therefore, batch yield must not be under 95% on the final reconciliation.
Output: Output through one shift on a single packaging line must be not less than 3500 units per day.
Non-conformance: Ensure no unnecessary changes occur during manufacturing or packaging processes without the approval of the Factory manager and ensure the approved changes are recorded on the relevant document.
Change Controls: If a manufacturing or packaging documents are requiring to have change during the production process the Assistant Factory Manager must fill a change control form with the required change to be matt and request approval from the Factory Manager before continuing with the change. If the requested change is successful the Factory Manager must update the specific production documents with the change.
Stock Control: The Assistant Production Manager must ensure on a quotably bass a stock count is performed in the R/Materials and components stores and the accuracy must be within 98%of Pastel accounting system.
Tableting Department
Yields: The tablet operator must achieve a batch yield of 98% from the theoretical batch document (Effective not more than 2% loss). Therefore, batch yield must not be under 95% on the final reconciliation.
Outputs: A single compression machine shift out per date must fall within 70,000 – 100,000 tablets.
Non-conformance: if during a compression process the tableting operator identifies that the product is not conforms to the product specifications it must not continue with the process and reported it to Assistant Production Manager until further instructions is given.
No reject batches: No rejected batches due to hardness, thickness, disintegration, friability or mass uniformity during the compression process.
Time keeping and breaks: compression operators must be present at the working place at all times during working hours (working hours are 8am to 4.3pm Monday to Thursday Friday 8am to 3pm tea time Monday to Thursday 10am to 10,15am Friday no tea).
Dress Code: The compression operators must have dressed in the appropriate clean room uniform and change the working shoes before entering the working place is strictly forbidden to wear the factory clothing or shoes outside the working place.
Accurate stock count: The compression operator is responsible for accuracy of table counting between theoretical and actual quantity specified on the document (the variance must note exceeded 2%)
Any other reasonable task: the compression operator may be requested by the Assistant Production Manager or Factory Manager to perform any responsible tasks required at Sparta Pharma.
Capsule Department
Yields: The encapsulating operator must achieve a batch yield of 98% from the theoretical batch document (Effective not more than 2% loss). Therefore, batch yield must not be under 95% on the final reconciliation.
Outputs: A single encapsulation shift out per date must fall within 60000 – 100000 capsules.
Non-conformance: if during an encapsulation process the encapsulating operator identifies that the product is not conforms to the product specifications it must not continue with the process and reported it to Assistant Production Manager until further instructions is given.
No reject batches: No rejected batches due to disintegration, or mass uniformity during the encapsulated process.
Time keeping and breaks: Encapsulation operators must be present at the working place at all times during working hours (working hours are 8am to 4.3pm Monday to Thursday Friday 8am to 3pm tea time Monday to Thursday 10am to 10,15am Friday no tea).
Dress Code: The encapsulating operators must have dressed in the appropriate clean room uniform and change the working shoes before entering the working place is strictly forbidden to wear the factory clothing or shoes outside the working place.
Accurate stock count: The encapsulating operator is responsible for accuracy of capsule counting between theoretical and actual quantity specified on the document (the variance must note exceeded 2%)
Any other reasonable task: the encapsulating operator may be requested by the Assistant Production Manager or Factory Manager to perform any responsible tasks required at Sparta Pharma.
Coating Department
Yields: The coating operator must achieve a batch yield of 99% from the theoretical batch document (Effective not more than 1% loss). Therefore, batch yield must not be under 95% on the final reconciliation.
Outputs: 1-2batches output on a single shift per day.
Non-conformance: if during a coating process the coating operator identifies that the product is not conforms to the product specifications it must not continue with the process and reported it to Assistant Production Manager until further instructions is given.
No reject batches: No rejected batches due to over spray the tablets or allow the tablets to run dry on the coating pan during the coating process.
Time keeping and breaks: Coating operators must be present at the working place at all times during working hours (working hours are 8am to 4.3pm Monday to Thursday Friday 8am to 3pm tea time Monday to Thursday 10am to 10,15am Friday no tea).
Dress Code: The coating operators must have dressed in the appropriate clean room uniform and change the working shoes before entering the working place is strictly forbidden to wear the factory clothing or shoes outside the working place.
Accurate stock count: The coating operator is responsible for accuracy of coated tables counting between theoretical and actual quantity specified on the document (the variance must note exceeded 1%)
Any other reasonable task: the coating operator may be requested by the Assistant Production Manager or Factory Manager to perform any responsible tasks required at Sparta Pharma.
Packaging Department
Yields: The packaging department operator must achieve a batch yield of 98% from the theoretical batch document (Effective not more than 2% loss). Therefore, batch yield must not be under 95% on the final reconciliation.
Outputs: Output 3,000-6,000 units on a single shift per day on a single line.
Non-conformance: if during a packaging operation the packaging operator identifies that the product or packaging components is not conforms to the product specifications it must not continue with the process and reported it to Assistant Production Manager until further instructions is given.
No reject batches: No rejected batches due to incurred count in the container, Incorrect cap used, incorrect label used, incorrect bottle used or incorrect tablet packed during the packaging operation.
Time keeping and breaks: Packaging operators must be present at the working place at all times during working hours (working hours are 8am to 4.3pm Monday to Thursday Friday 8am to 3pm tea time Monday to Thursday 10am to 10,15am Friday no tea).
Dress Code: The packaging operators that working in the primary they must dressed in the appropriate clean room uniform and change the working shoes before entering the working place is strictly forbidden to wear the factory clothing or shoes outside the working place. The packaging operators that working in the secondary areathey must dressed in the appropriate clean room uniform before entering the working place is strictly forbidden to wear the factory clothing outside the working place.
Accurate stock count: The packaging operator is responsible for accuracy of tables counting between theoretical and actual quantity specified on the document (the variance must note exceeded 1%)
Any other reasonable task: the packaging operators may be requested by the Assistant Production Manager or Factory Manager to perform any responsible tasks required at Sparta Pharma.
Accountin
Gross margin: As a % of selling price – The average Gross profit margin per product must not be less than 20%
Debtor’s management: Debtor’s age analysis must be sent to the CEO before the 3rd day of each month for review. Statements must be forwarded to customers no later than the 1st day of each month.
Creditor’s Management: Creditor’s age analysis must be sent to the CEO before the 7th day of each month for review. Statements must be received from suppliers no later than 5th day of each month.
Debtors Management: Once the debtor’s statements are sent out, the Financial Manager will send put a first request for payment to replenish cash flow. If an account is not settled in a timely manner, the manager will then make a second request for payment telephonically until payment is received. The company has a Nil provision doubtful debt as it the opinion of the finance department, that all debts are fully recoverable.
Creditors management: Any unreconciled items are reconciled between the company’s bookkeeper and the supplier’s accounting department.
Administration
Sales quotations: Once the product coasting has been received from the Chief Executive Officer, a sales quotation should be sent to the customer within 48 hours.
Cycle time of purchase order: The time taken for the Procurement personal to send a requisition for a Purchase order to the Administration department and then receiving it back to forward onto the supplier must not exceed 48 hours.
Data capturing: Capturing of all components batch manufacturing documentation into Pastel must be completed within 48 hours. This will prevent Pastel from booking stock which doesn’t exist and appropriating it to further batches.
Stock Control on pastel: The administration department must ensure that the Pastel system is accurate within 99% on each raw material and component when compared to actual physical stock count received from the Factory Manager. Non-conformances must be reported to the Factory Manager.
On-time invoicing: The administrator department must ensure that a copy of the invoice and delivery note must be sent to the customer within 48 hours of the batch completion. More specifically the invoice must be received prior to the consignment arriving with the customer.
Artwork and Design Manager
Packaging artwork: The artwork and design manager must receive a Label spec document from the Chief Executive Officer prior t commencement of label design
Artwork lead time: A theoretical lead time must be communicated to the Chief Executive Officer and monthly updates must follow as to the progress and estimated time completion.
Print: Print ready artwork must be kept on file and sent to the Factory Manager to include in the product must file.
Formulation
Turning your product idea into an opportunity with viable product formulation taking into account your budget, target audience and required dosage.
Procurement
Raw material procured from ISO9001 validated global suppliers.
Packaging
From concept to mock-up creation, for all types of packaging requirements.
Design
Creating a unique and established shelf ready designed package ready for market.
From digital to a shelf ready solution, with years of experience, our accredited printers are able to supply most substrate and finish requirements.
Quality Assurance
Comprehensive Quality Control from start to finish.
Team Members
Our management structure with a combined 80 years of industry experience allows us to understand what it takes to bring your product to market at the best possible price, providing a quicker than market average turnaround time whilst maintaining the highest quality assurance levels possible.
Our staff complement of 70 members is growing each quarter and we are fully geared to take your product and business to new heights.